Workholding for Hard-to-Clamp Parts: Thin-Wall, Delicate & Irregular
Every shop hits them eventually: the part that rings like a bell, the casting with no flat face, the thin-wall tube that collapses the moment a jaw touches it. These are the jobs that turn a confident setup into an hour of shims, tape, and prayer. The good news — modern workholding has specific answers for each failure mode. This guide maps the part problem to the right clamp.
If you have not yet standardized your vise, our Self-Centering vs Traditional Vise comparison and the 5-Axis Workholding guide cover the foundations this builds on.
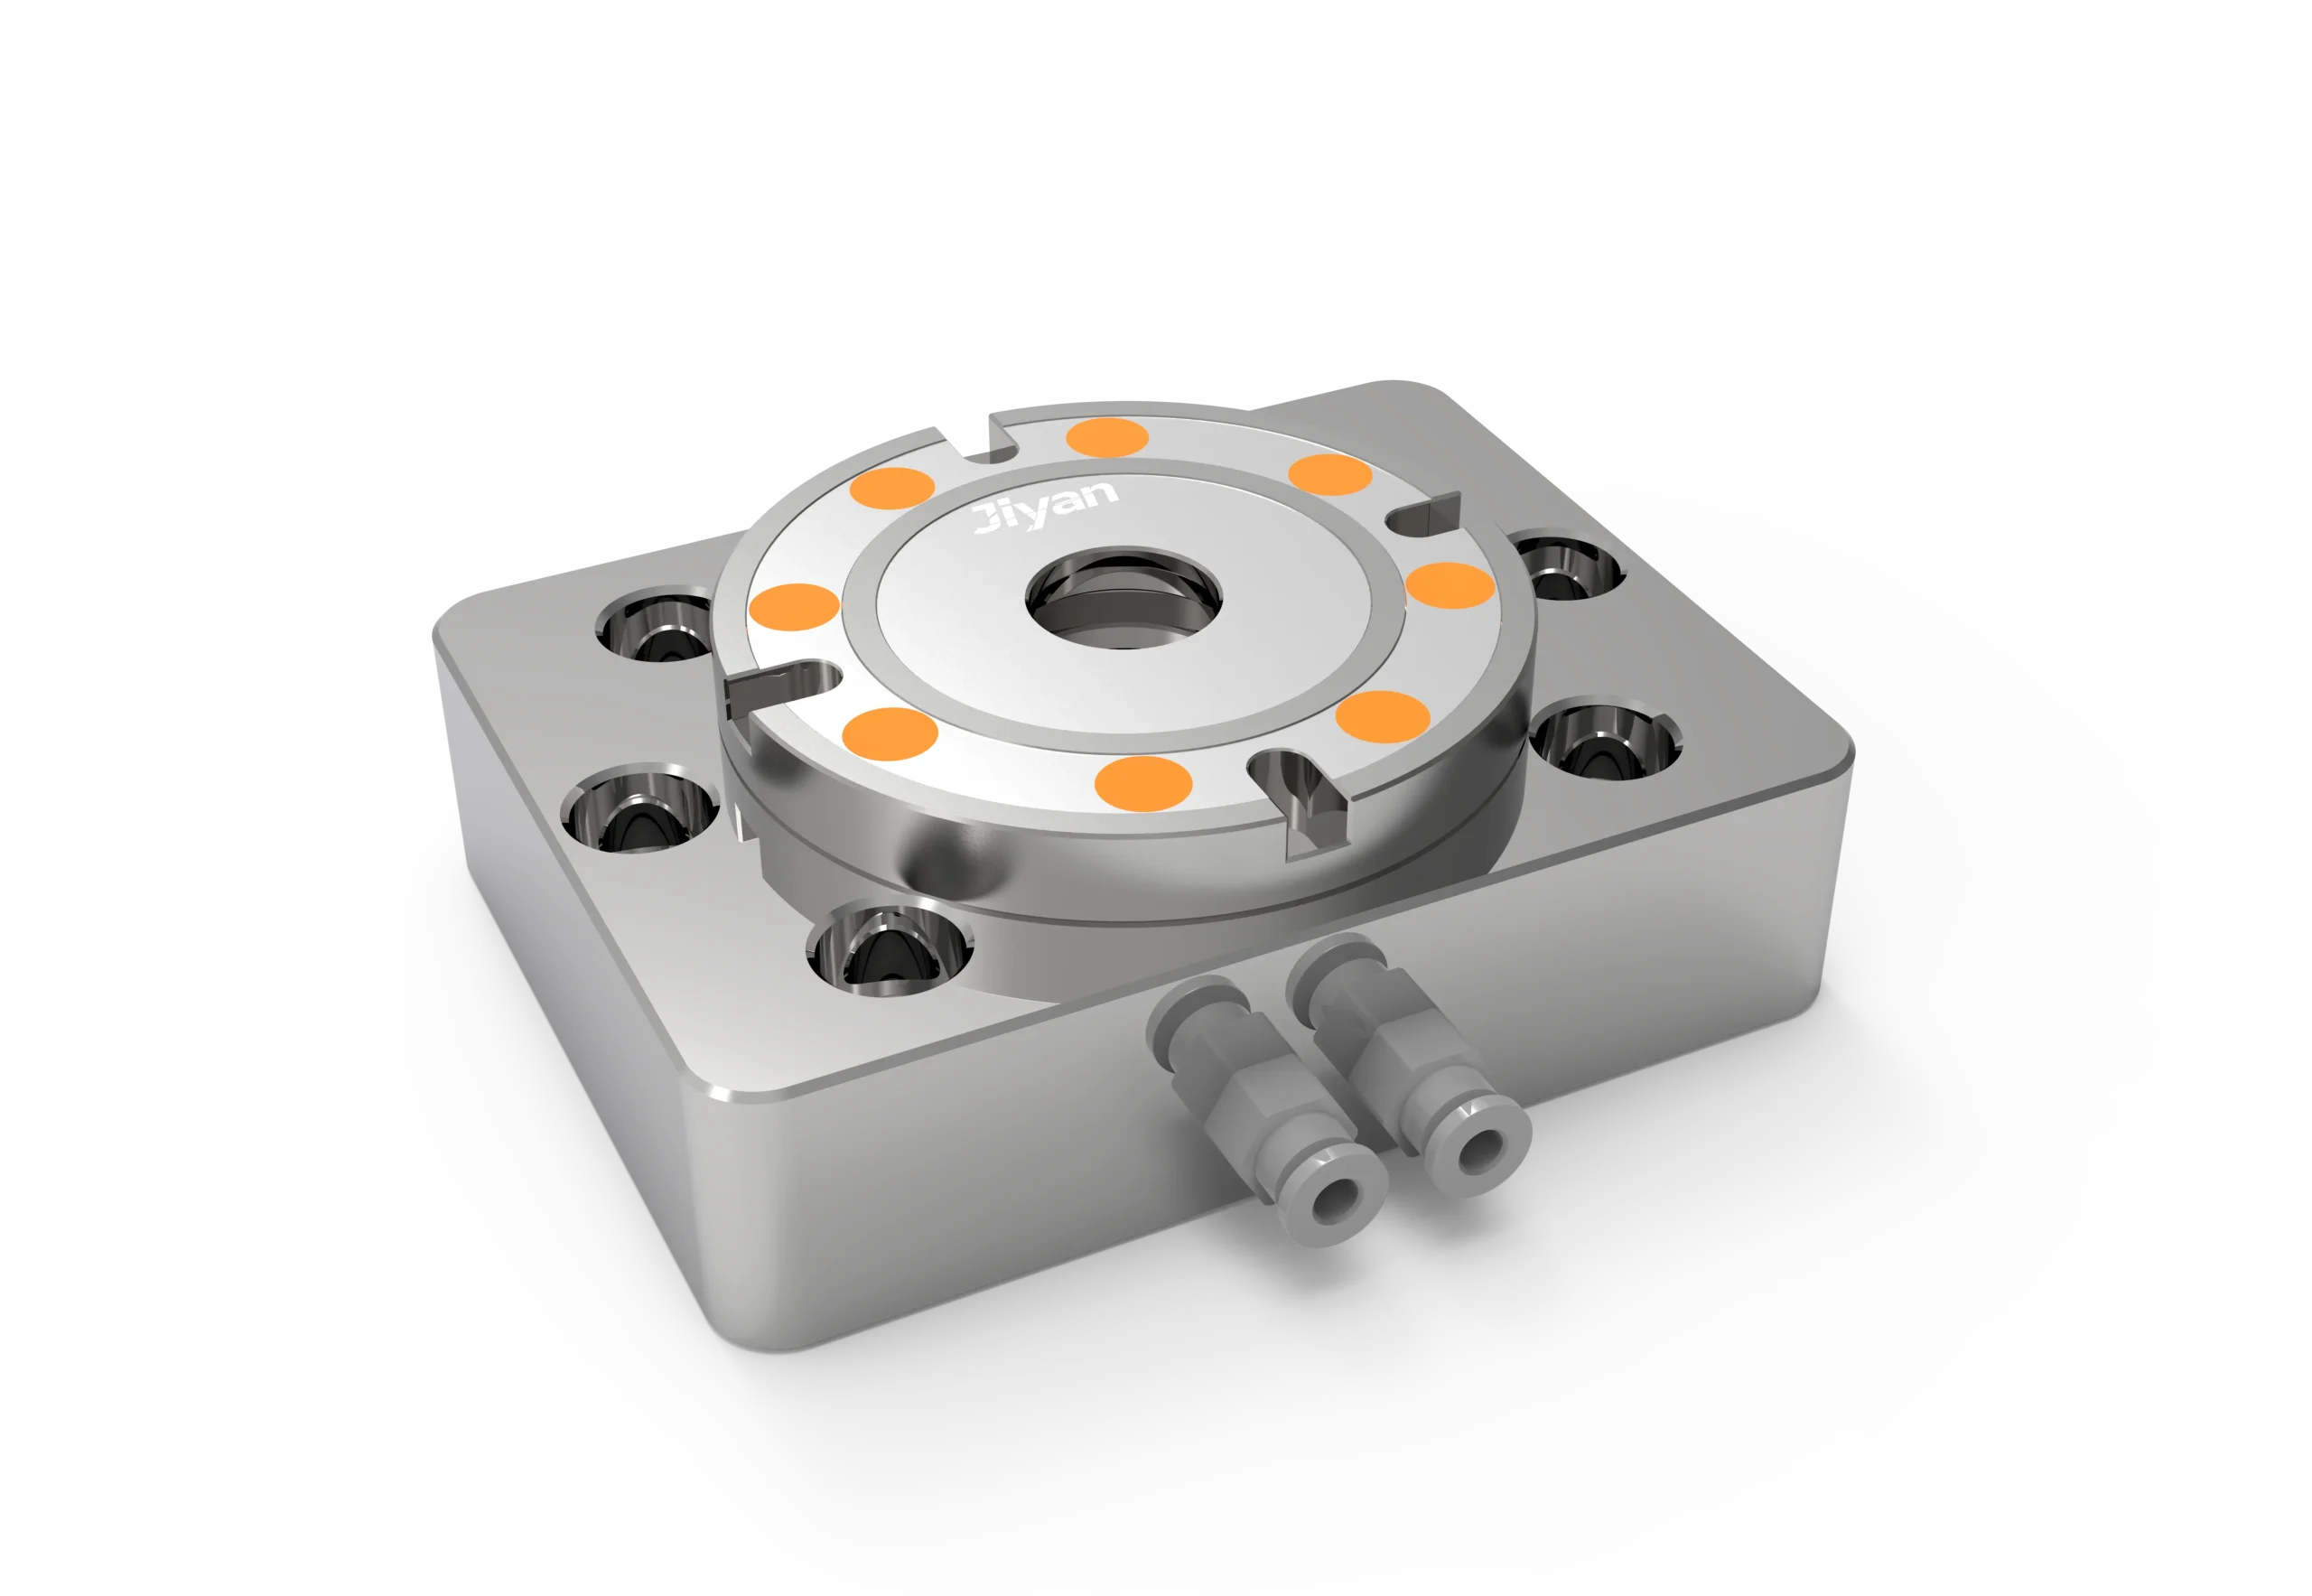
Self-centering grip is the first answer for delicate and irregular parts — equal force from both sides.
01 Name the failure mode first
"Hard to clamp" is not one problem; it is four, and the fix for one can ruin another:
- Distortion — you hold it square, it springs, you machine it, it relaxes out of tolerance.
- No datum — the part has no flat, stable face to locate against.
- Low rigidity — it chatters or rings because the clamp point is far from the cut.
- Fragility — the surface itself cannot take point load without marking or crushing.
Pick the dominant failure mode before you pick the vise. Most "hard" parts have one clear culprit.
02 Thin-wall parts: distribute, don't squeeze
Thin-wall tubes, housings, and sheet all fail by distortion. The instinct — clamp harder — is exactly wrong; more force just deforms more.
The answer is full-surface, equalized grip:
- A self-centering vise pulls the part to its own centerline with balanced force, so it does not bow sideways.
- Wrap the jaw in a soft jaw (aluminum or copper) so load spreads over a wide arc instead of two points.
- Clamp on a feature that is not the tight-tolerance wall — grip the flange, machine the tube.
"Rule
If you can deflect the wall with a finger, you are clamping too hard or in the wrong place. Move the grip to a stiffer section and let the thin wall float free.
03 Delicate and finished surfaces: soft jaws and full support
A machined or plated surface cannot take a hardened serration. Two moves fix it:
- Soft jaws — mill the jaw to the part's contour so contact is conformal, not point. The part feels supported because it is.
- Support behind the cut — chatter is a stiffness problem. A steady rest, a sub-jaw, or a locating pin on the far side of the feature kills the ring.
This is where a self-centering pneumatic vise earns its keep: equalized grip means the finished face is never squeezed asymmetric.
04 No flat datum: locate on features, not faces
Castings, forgings, and 3D-printed blanks often have no usable flat. Stop trying to find one. Instead:
- Locate on a bore or a boss with a pin or a expanding collet — the part's own feature becomes the datum.
- Use a zero-point base to lock a pre-located fixture: you indicate the fixture once, then every raw blank drops into the same known position. Our Quick-Change Zero-Point guide walks through building that library.
- Magnetic or vacuum tables for very thin, very flat stock where mechanical grip would distort it.
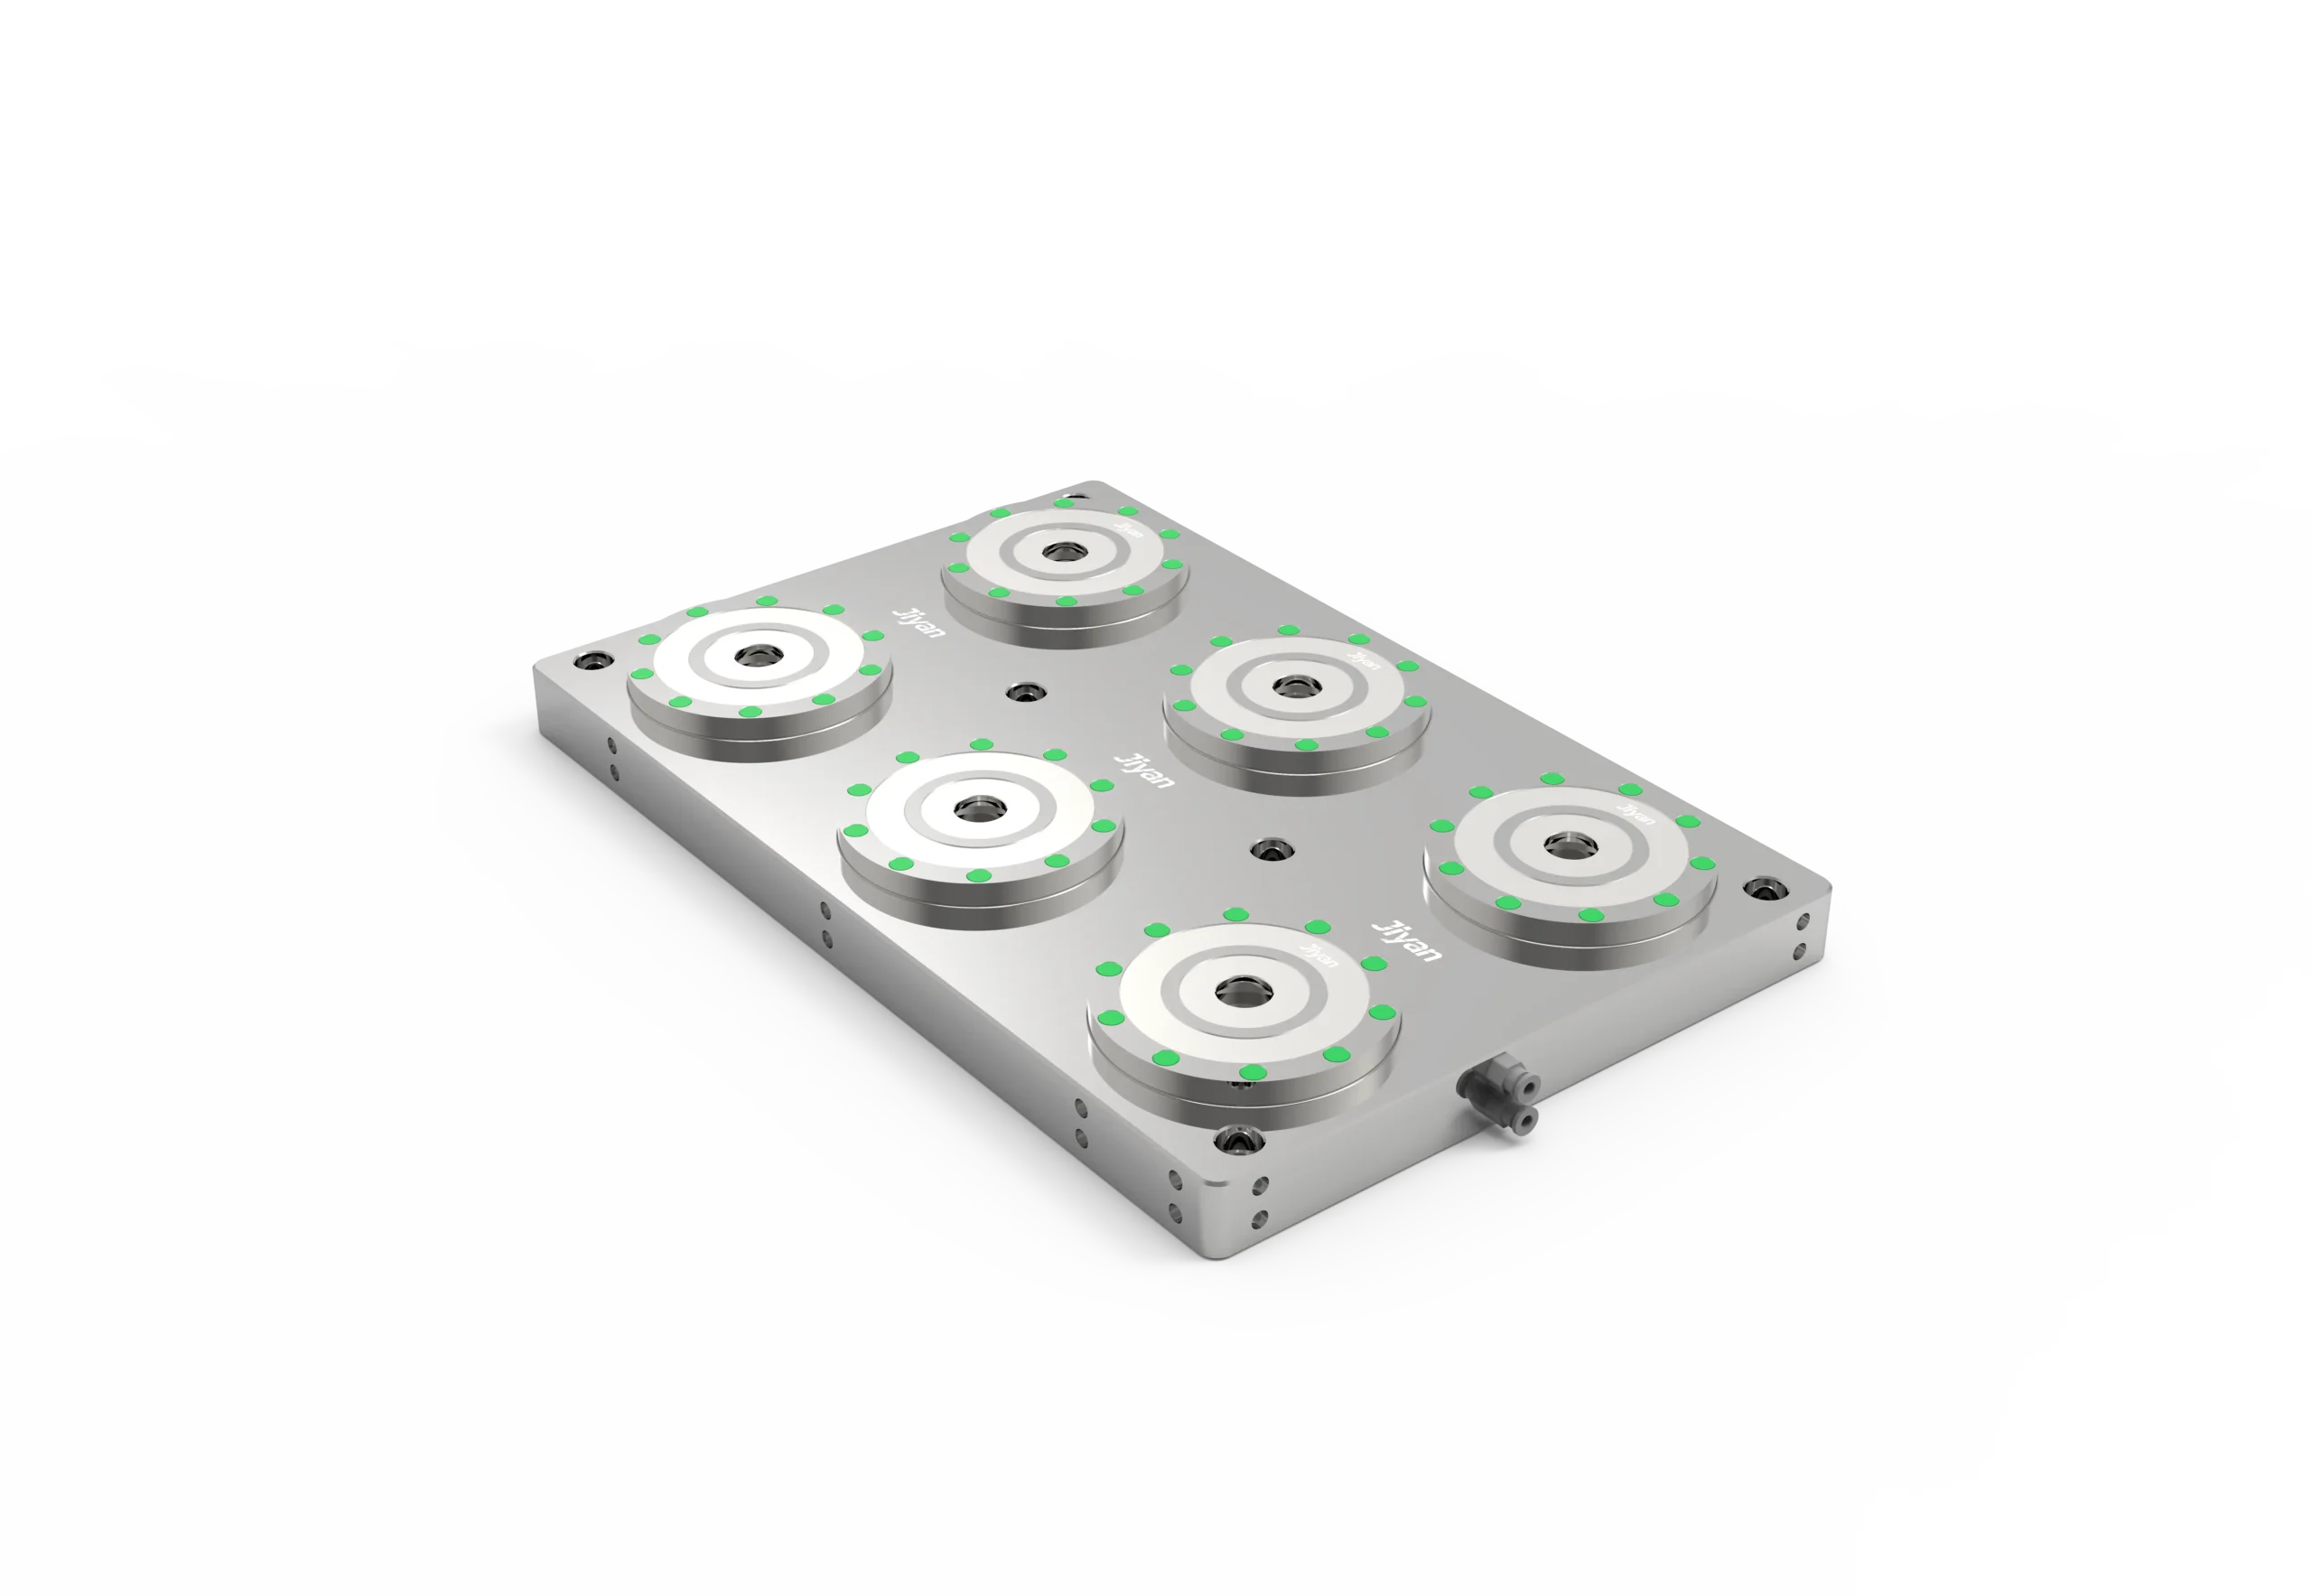
Multi-station clamping turns a tray of awkward small parts into one repeatable setup.
05 Small and batch parts: clamp many at once
Tiny parts are hard because the vise is bigger than the work. The fix is density:
- Multi-station vises hold six or more parts in one mounted unit, so you machine a whole row instead of one.
- Palletize the lot: one fixture, many raw blanks, swap the pallet instead of re-fixturing each part.
- Keep the locating faces identical across stations so a single offset corrects the whole batch.
This collapses setup time and removes the per-part variation that makes small parts frustrating.
06 Irregular and 5-axis parts: hold the base, cut the top
When the part needs cutting from multiple angles, you cannot clamp the top. The strategy is to grip a stable base and let the part stick up into the envelope:
- A zero-point base anchors a dedicated fixture or a dovetail blank; the part is pre-located and the spindle reaches all sides.
- Dovetail clamps bite a small undercut at the base — minimal contact, maximum access, no top interference.
- Tombstones and trunnions hold several fixtures at once for true unattended multi-face machining.
The 5-axis workholding solutions guide goes deeper on interference and rigidity for these setups.
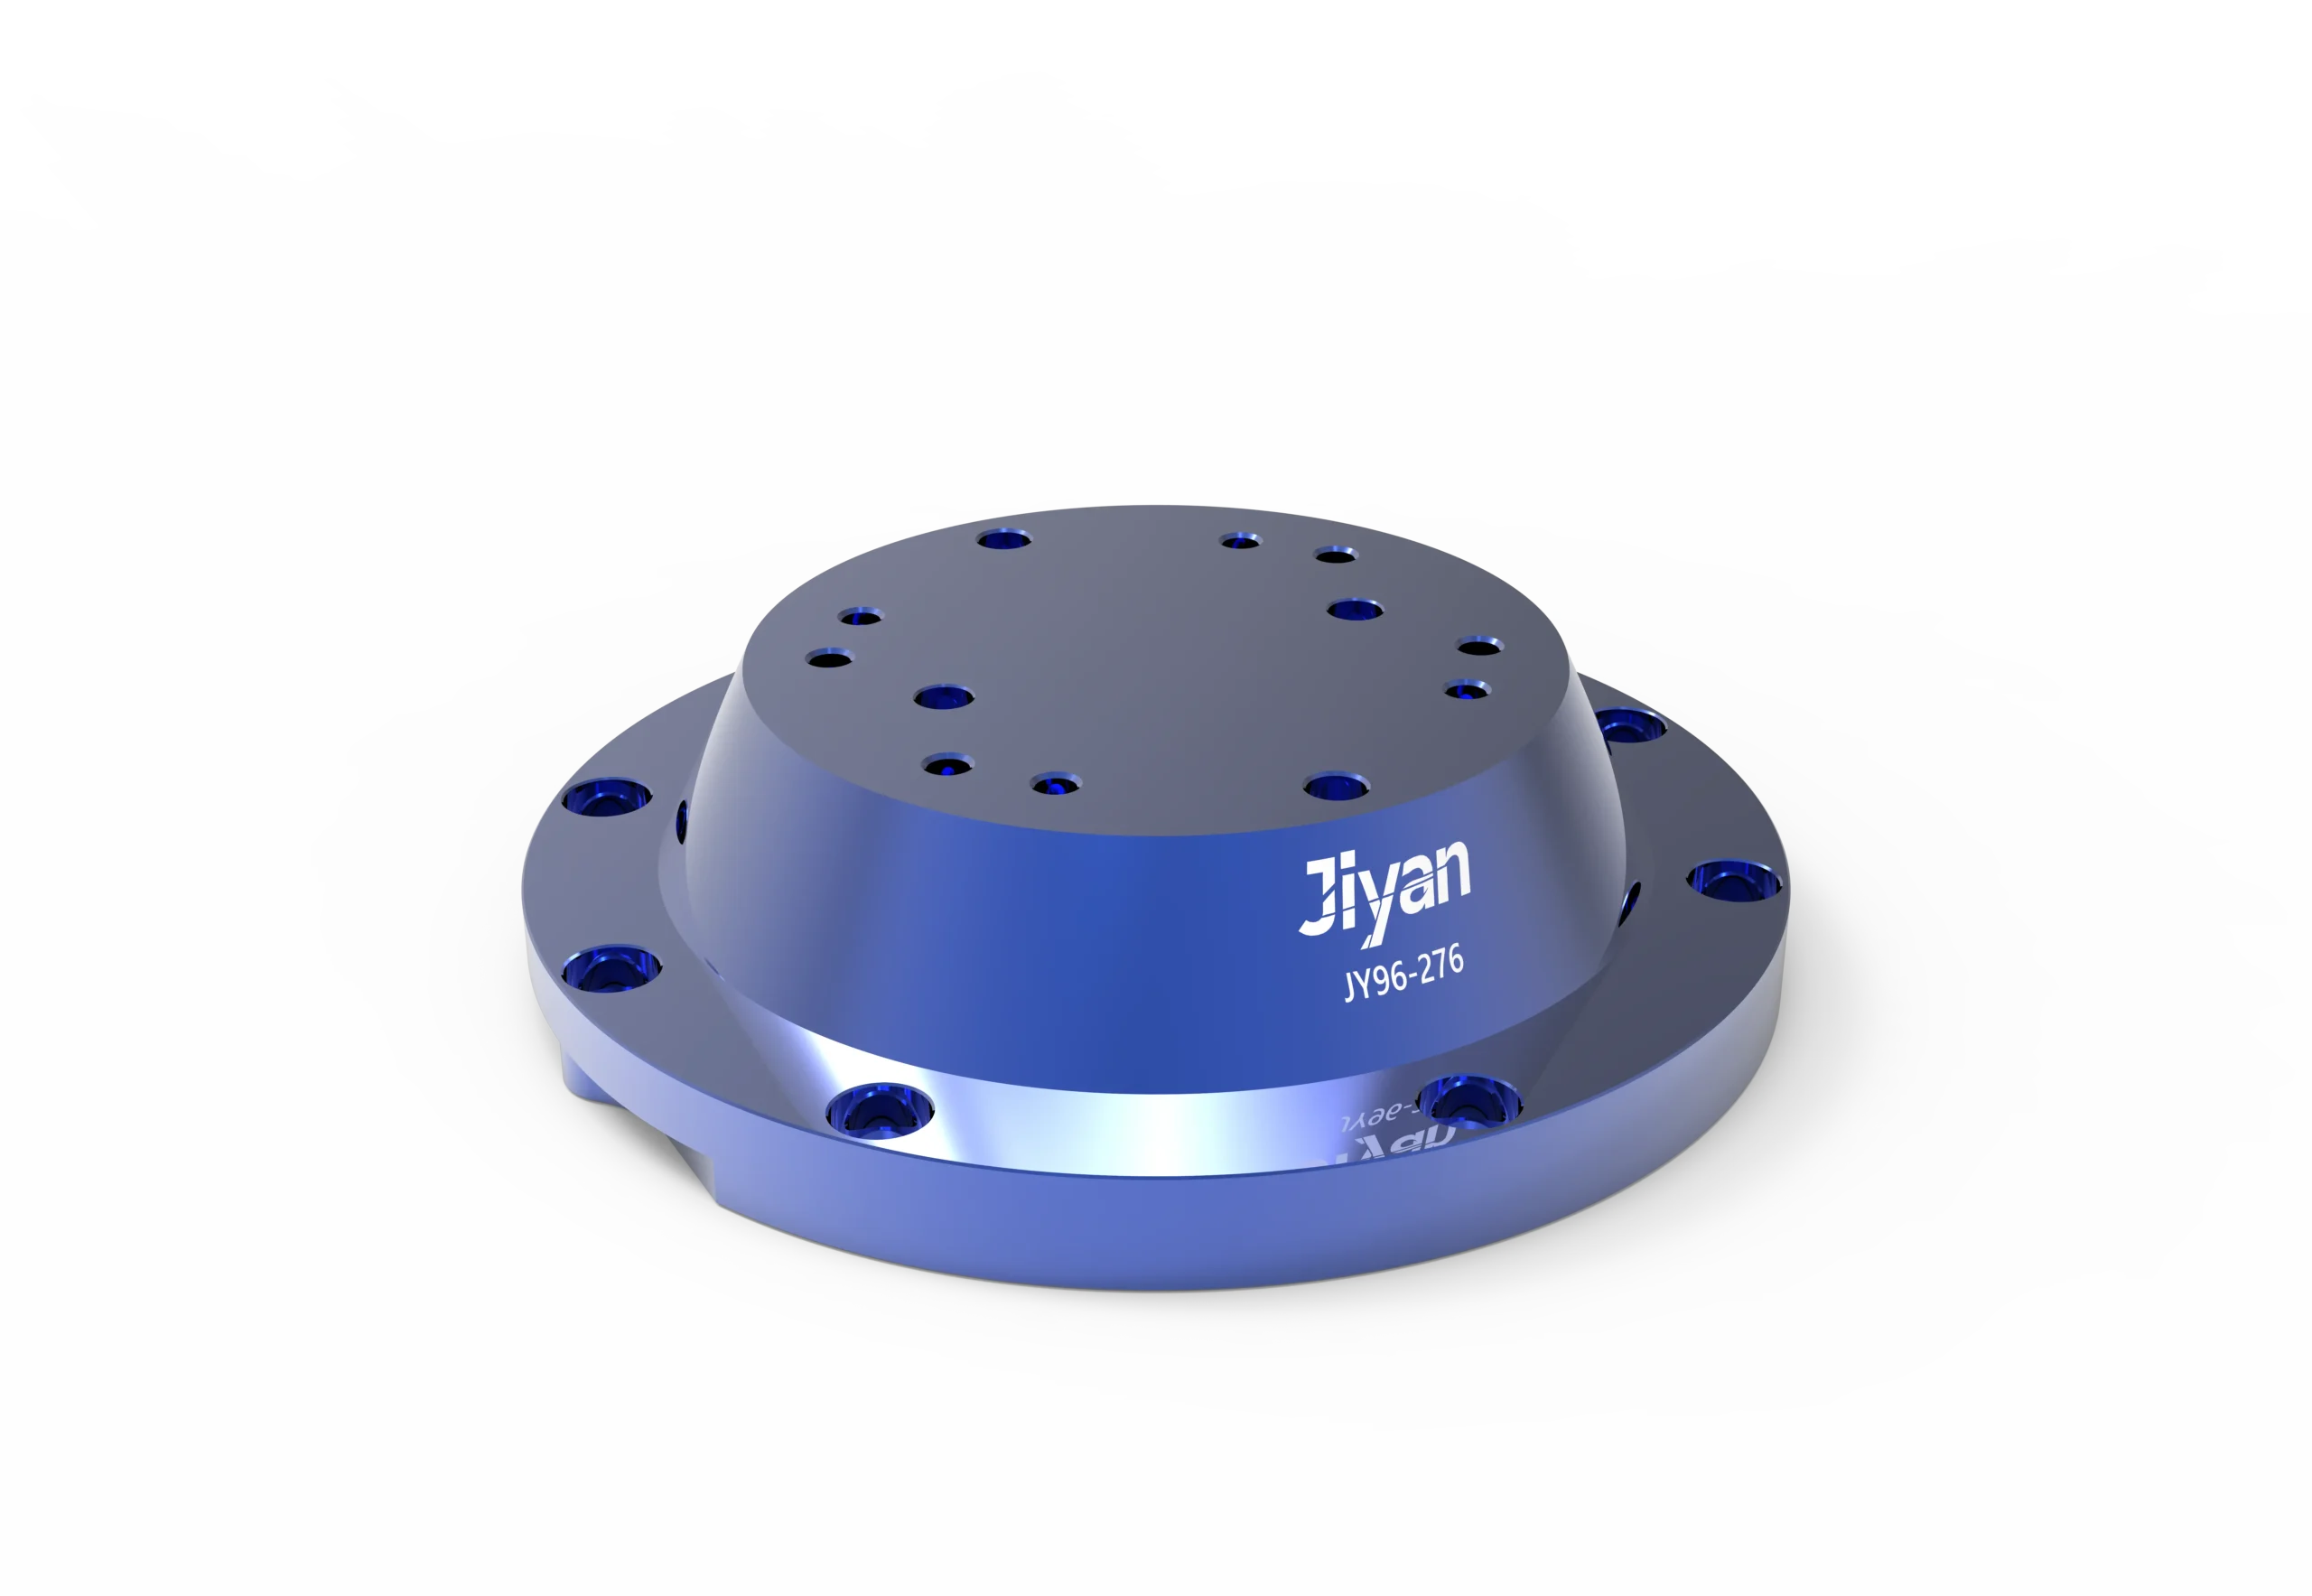
The TS96-276 zero-point base — lock a fixture once, swap parts against a known datum.
07 The zero-point shortcut for everything awkward
The single biggest lever for hard parts is decoupling locating from clamping. A zero-point clamping system does exactly that:
- Build the tricky fixture once, indicate it once, lock it to the base.
- Every subsequent raw part inherits that datum in seconds, with sub-5-micron repeatability.
- The vise becomes a stable platform; the fixture does the hard locating.
For low-volume, high-variety work this is the difference between a one-off scramble and a repeatable process.
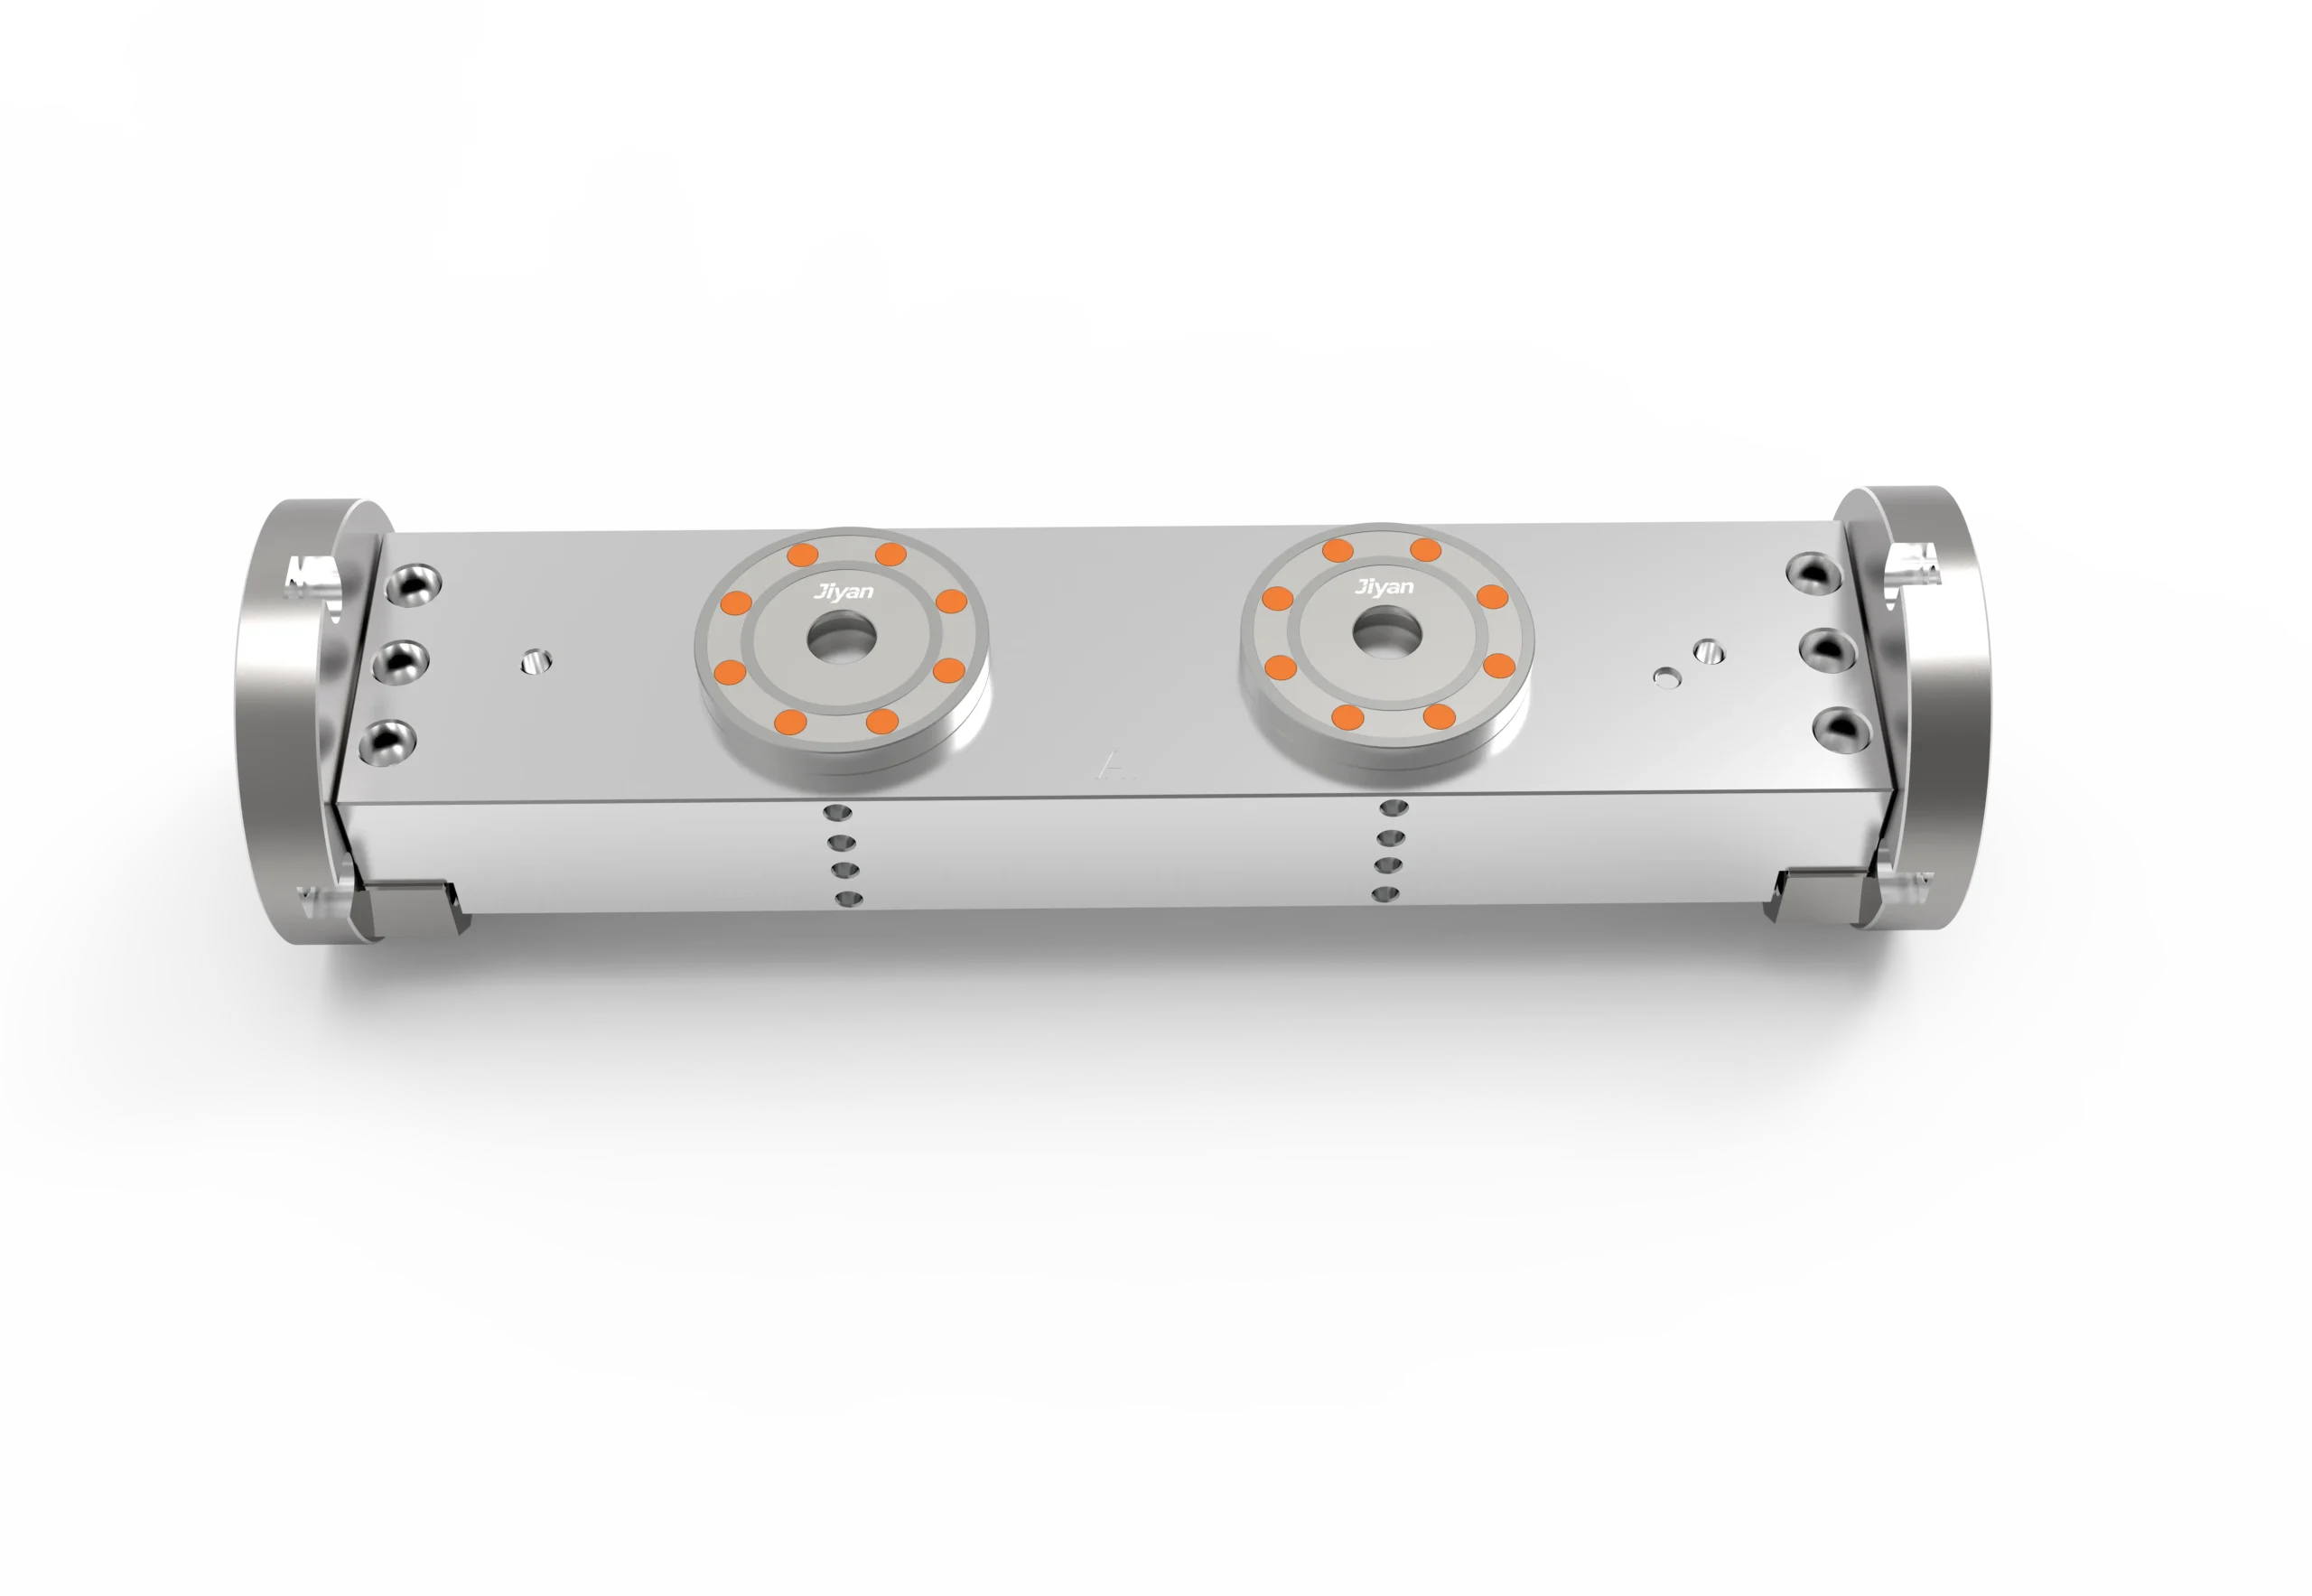
Double-sided zero-point pallets let you fixture both faces offline and flip in seconds.
08 A decision matrix
| Part type | Dominant problem | Best clamp |
|---|---|---|
| Thin-wall tube | Distortion | Self-centering + soft jaws, grip the flange |
| Finished/plated | Fragility | Conformal soft jaws + back support |
| No flat datum | Locating | Pin/bore locate, zero-point fixture |
| Tiny/batch | Density | Multi-station or palletized vise |
| 5-axis/irregular | Access | Zero-point base + dovetail/tombstone |
| One-off weird | All of them | Build a zero-point fixture once |
09 Common mistakes
- Clamping harder to stop chatter — adds distortion, rarely helps. Add support instead.
- Locating on the feature you are about to machine — you are measuring what you destroy. Locate upstream.
- Ignoring part spring — indicate after clamping, not before. What moves, moves.
- Custom fixture for a one-off — a zero-point base with a quick soft-jaw setup beats a machined fixture you use once.
10 Start simple, scale to zero-point
You do not need a full pallet library on day one. Most shops progress:
- Self-centering vise + soft jaws solves 70% of delicate and irregular parts.
- Multi-station vise absorbs the small-batch work.
- Zero-point base + one fixture handles the truly awkward, multi-face jobs.
Each step reuses the last — soft jaws fit the self-centering vise, the vise mounts on the zero-point base.
11 Bottom line
Hard-to-clamp parts are rarely a force problem; they are a locating and distribution problem. Equalize the grip, locate on the part's own features, support behind the cut, and when volume or variety justifies it, decouple locating from clamping with a zero-point system. Do that and the "impossible" part becomes just another setup.
Stuck on a specific part? Send JIYAN the drawing and we will suggest the clamping approach and the exact vise to match.
For more fixture strategies that survive full five-axis motion, continue with the 5-axis workholding guide.